Bigger Is Not Always Better in Production Planning
When manufacturers compare equipment quotations, capacity is often one of the first numbers they look at.
A 1-ton-per-hour line appears attractive until a 3-ton-per-hour system is compared.
Then a larger system appears more impressive.
But production capacity is only useful when it matches the rest of the business.
A machine that can theoretically produce a large volume does not automatically make a project more profitable.
The factory still needs enough raw material, storage, drying capacity, packaging speed, operators, power and market demand.
This is particularly important for sawdust cat litter and wood-based animal bedding because raw material can be bulky and variable.
Capacity Should Begin With Raw-Material Availability
Imagine a factory that has access to 20 tons of usable sawdust every working day.
That figure creates a practical ceiling for production.
There is no reason to install a sawdust cat litter production line that requires much more feedstock than the factory can reliably supply.
The calculation should consider:
- Daily available material
- Moisture content
- Working hours
- Seasonal availability
- Storage losses
- Material already committed to other customers
Raw-material supply should be measured over a realistic period rather than estimated from a single good day.
Then Consider Market Demand
The second part of the equation is sales.
A new manufacturer may have abundant sawdust but no established market for the finished litter.
Starting with excessive production capacity can create large stocks of unsold product.
This can tie up capital in:
- Raw materials
- Finished inventory
- Packaging
- Warehouse space
- Energy
- Labor
A phased approach may make more sense.
Start with a realistic commercial output, learn the market and expand as demand becomes measurable.
Capacity Is Also About Operating Hours
Two factories may both advertise a 2 T/H production line but have completely different monthly output.
One may run 8 hours per day.
Another may run 16 hours.
Another may only operate one shift because of electricity cost or labor availability.
Therefore, “tons per hour” should always be converted into a realistic monthly production target.
A simple project calculation should include:
Hourly output × operating hours × working days × expected utilization.
The final result is much more useful than a headline capacity number.
Why Animal-Bedding Equipment Can Be Relevant
Although cat litter has specific requirements, the underlying biomass forming technology may overlap with other bedding products.
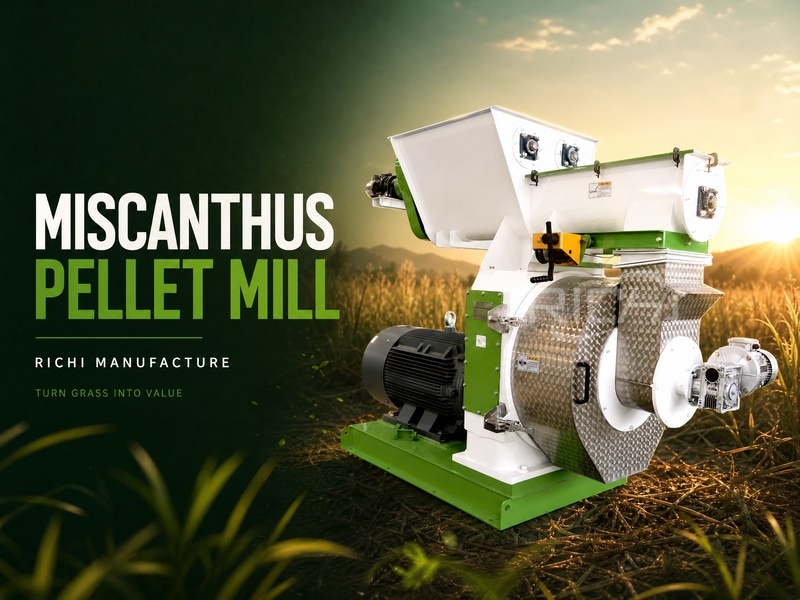
A manufacturer researching a industrial animal litter pellet machine for sale may be considering equipment not only for cat litter but also for other animal-bedding applications.
That can be useful when the business plans to diversify.
For example, a wood-residue processor may want to produce cat litter for the retail market while also serving agricultural customers with bedding products.
The equipment configuration should reflect that strategy.
Don’t Forget Moisture Reduction
Production capacity is also affected by how much water must be removed.
Wet sawdust contains more weight before drying but less weight after moisture reduction.
This means that raw-material tonnage cannot be directly compared with finished-product tonnage without accounting for moisture.
The more moisture that must be removed, the greater the drying demand.
That can influence:
- Dryer size
- Heat consumption
- Residence time
- Cooling demand
- Operating cost
A capacity study should therefore start with material condition, not only machine output.
A High-Capacity Forming Machine Can Still Have Low Real Output
A machine may be designed for a certain nominal throughput, but actual production can be lower when:
- Feed material is too wet
- Particle size is inconsistent
- Raw material contains oversized chips
- Feeding is unstable
- The product specification is demanding
- The operator needs frequent adjustments
This is why test data and material-specific calculations are more valuable than generic catalogue numbers.
A machine should be judged under conditions similar to the planned factory.
Think About the Dryer as a Bottleneck
The dryer is particularly important in biomass processing.
Suppose the forming section can produce 4 T/H.
If the drying section can only stabilize 2 T/H under actual conditions, then the entire factory operates closer to 2 T/H.
The same principle applies to cooling and screening.
The line capacity is determined by the practical performance of the limiting stage.
This is one reason a complete engineering calculation is more useful than purchasing each machine separately.
What Does a Balanced Line Look Like?
A balanced production system should maintain reasonable continuity between stages.
For example:
Raw material preparation → forming → drying → cooling → screening → packaging
Each section should be capable of supporting the next.
Material should not accumulate excessively between machines.
The factory should also have enough buffer capacity to handle short fluctuations without stopping the entire line.
This is especially valuable in continuous industrial production.
Different Customers May Need Different Capacities
The ideal capacity can differ by customer type.
Small woodworking factory
The primary goal may be to add value to existing residues.
Dedicated pet-litter producer
The focus may be on stable retail supply and packaging efficiency.
Biomass-processing company
The company may want a flexible system serving several applications.
Large industrial manufacturer
The focus may be on automation, high throughput and consistent output.
The equipment selection should reflect the business model.
Production Capacity Should Leave Room for Product Development
Manufacturers often start with one product formula.
After entering the market, they may develop additional products.
These could include:
- Different particle sizes
- Fragranced varieties
- Premium low-dust products
- Lightweight products
- Different packaging formats
A line designed with some flexibility can make these changes easier.
The machine should not necessarily be dedicated to only one narrow operating condition unless that specialization is commercially justified.
The Value of Modular Expansion
One useful strategy is designing the plant in modules.
For example, a company may start with a moderate-capacity forming section and later increase total production by adding parallel equipment.
This can be easier than replacing a complete production line.
Expansion planning may include:
- Reserved floor space
- Spare electrical capacity
- Larger material storage
- Extendable conveyors
- Modular packaging
- Flexible control architecture
The goal is to avoid rebuilding the factory from scratch when demand increases.
Energy Consumption Should Be Considered Early
Equipment capacity is strongly connected to energy requirements.
Drying often consumes more energy than customers expect, especially when raw material enters the plant with substantial moisture.
Energy planning should include:
- Heat source
- Fuel availability
- Electricity price
- Motor load
- Operating hours
- Seasonal conditions
A larger plant may benefit from better energy utilization at scale, but only when capacity is actually used.
Capacity and Labor Are Connected
A highly automated line may require fewer operators than a manually controlled system, but maintenance and quality-control responsibilities still remain.
The factory should define:
- Number of operators per shift
- Maintenance responsibilities
- Quality-control staff
- Packaging labor
- Forklift requirements
These costs should be included in the project evaluation.
What About Packaging Capacity?
Packaging is often overlooked during equipment selection.
Suppose a production line generates 4 tons of finished litter every hour, but the packaging system can only handle 2 tons.
The production line cannot maintain continuous output.
Packaging can therefore become the final bottleneck.
Bag size also changes the number of packages per hour.
Smaller bags require more filling and sealing cycles.
Larger bags may reduce packaging frequency but increase manual-handling requirements.
The product strategy should determine the packaging configuration.
Capacity Should Be Evaluated With Product Quality
Increasing production speed can affect quality.
For example, a process running near the upper limit may produce more fines, less stable particles or inconsistent moisture.
The right capacity is therefore not necessarily the maximum achievable output.
A better definition is:
The highest output that can be maintained consistently at the required product quality.
That definition is much more meaningful for a consumer product.
How Technical Suppliers Fit Into the Decision
A supplier should be able to translate the customer’s raw material and product requirements into an equipment configuration.
That may include:
- Milling
- Feeding
- Forming
- Drying
- Cooling
- Screening
- Packaging
A company such as Richi manufacture can be included in the supplier research process, especially when comparing equipment packages for biomass and animal-bedding applications.
Still, buyers should compare technical proposals according to actual project conditions rather than simply comparing brands.
A Simple Capacity Checklist
Before accepting an equipment quotation, ask:
What raw material was used for the calculation?
What moisture level was assumed?
What finished-product specification was used?
What operating hours were assumed?
What is the expected actual output?
What is the capacity of the dryer?
What happens to fines and oversize product?
What packaging speed is required?
Can the line be expanded later?
The answers reveal whether the capacity number represents a realistic project scenario.
Capacity Should Support the Business, Not Define It
A successful factory does not exist to keep machines busy.
It exists to produce a product that customers will buy consistently.
That means capacity should follow the business strategy.
A small line can be highly effective when it matches demand and raw-material supply.
A large line can also be appropriate when the company has strong sales channels, sufficient feedstock and the infrastructure to support continuous operation.
For further reading on production planning and equipment comparison, look at this website for additional industry information.
Conclusion
Choosing capacity is one of the most important decisions in a sawdust-based litter project, but it should never be made from a single machine specification.
The right capacity comes from balancing raw-material supply, product demand, moisture removal, forming performance, drying, cooling, screening, packaging and future expansion.
Manufacturers that define these factors before purchasing equipment usually have a clearer understanding of what they actually need.
The goal is not to buy the biggest machine.
The goal is to build a production system capable of delivering the right amount of product, at the right quality, under real operating conditions.